A bonded fleece windproof jacket supplier for laminate engineered outerwear
RB Advertising builds bonded fleece windproof jackets to your laminate specification, not from a fixed catalogue. Your technical team defines the outer face, the barrier film, the inner fleece, and the bond system, and our cut and sew floor in Tagum City and Cagayan de Oro produces the programme in house. This page covers how the laminate is built and specified.
- 20 PiecesLow MOQ
- 200 to 300 GSMFleece weights
- 3 LayerBonded laminate
- 7 to 12 DaysBulk production
Three layer cross section
- Layer 1, outer face
- Dense knit, micro polar, or grid fleece. Specified on your tech pack.
- Layer 2, barrier film
- Windproof membrane film, or a breathable membrane where vapour transfer matters.
- Layer 3, inner face
- Micro fleece, grid fleece, or sherpa backer. Specified on your tech pack.
Thickness and weight are not published here. The laminate is built to the construction and fleece weight on your tech pack.
Key specification rows
- Construction
- 3 layer bonded laminate
- Outer face
- Dense knit, micro polar, or grid fleece
- Barrier
- Windproof film, breathable membrane on request
- Inner face
- Micro fleece, grid fleece, or sherpa
- Bond method
- Controlled heat and pressure lamination
- Fleece weight
- 200, 260, 280, or 300 GSM
- Hardware
- SBS zippers
- Branding
- Tajima embroidery and private label finishing
- Testing
- Third party laboratory on request
- In house bonding and cut and sewJoined, cut, and sewn in house.
- Built to your specificationFaces, film, and bond system from the tech pack.
- Third party testing on requestArranged for a programme.
- OEM and private label finishingNeck labels and branded packaging.
How a bonded windproof fleece laminate is built
Bonding joins the outer face, the barrier film, and the inner fleece into a single panel using an adhesive system under controlled heat and pressure. The bond runs across the full surface rather than along a seam, so the three layers behave as one fabric with no quilting lines and no needle channels for wind to pass through.
Outer face, barrier, and inner face
The outer face is the surface a buyer sees and your branding sits on. A dense knit gives a smooth, print ready face, micro polar gives a softer hand, and grid fleece gives a technical texture. The barrier film sits in the middle and does the wind blocking. The inner face touches the body and controls the feel and the moisture handling. The three layers are matched rather than mixed at random, so a dense knit outer with a micro fleece backer reads clean on a corporate programme, while a micro polar outer with a grid fleece backer balances warmth with faster drying. Review the range alongside our polar fleece jacket manufacturing and softshell programmes.
| Outer face | Barrier | Inner face | Resulting behaviour |
|---|---|---|---|
| Dense knit | Windproof membrane film | Micro fleece backer | Smooth print ready face with a brushed backer. Balanced warmth for corporate and retail programmes. |
| Micro polar | Windproof membrane film | Micro fleece backer | Softer hand and higher loft. A warmer surface for cold exterior use. |
| Grid fleece | Breathable membrane film | Grid fleece backer | Open channel inner to move vapour during active work. Suited to mid layer and technical use. |
| Dense knit | Windproof membrane film | Sherpa pile backer | Heaviest thermal band in the range. Cold storage, highland crews, and winter export. |
| Micro polar | Windproof membrane film | Grid fleece backer | Warm outer with a lighter, faster drying inside. Mixed climate programmes. |
Delamination control on a bonded laminate
Delamination happens when the adhesive bond between the layers fails and the faces begin to separate. A technical buyer should understand the causes before the programme is priced, because the fix sits in the specification, not in the final inspection.
- Heat exposure: sustained heat can soften the adhesive before the laminate has fully cured.
- Low grade adhesive: an adhesive not matched to the faces bonds weakly from the first run.
- Washing cycles: repeated domestic washing stresses every layer of the bond.
How it is guarded in production
We control the lamination temperature and pressure to the adhesive system, so the bond forms in the window the adhesive needs. Before the bulk run we complete a bonding trial on the actual faces and confirm the construction with your team, then allow the full cure time before cutting begins. We can also arrange third party laboratory assessment where a buyer wants an independent record.
What the buyer should put in the tech pack
- Membrane or film type and whether breathability is required
- The adhesive expectation, such as film or dot bond
- A bond peel strength target and the test method to report it
- The wash care the programme must survive
Standard test methods a buyer can request
We do not publish test results here, because a result depends on the exact fabric and construction in your programme. These are the standard methods a buyer can request, and third party laboratory testing can be arranged on request for a programme. Reports are issued by the testing laboratory, not by us.
- ISO 811
Hydrostatic head
Measures the water pressure a fabric resists before water passes through.
- ASTM D737
Air permeability
Measures the air that passes through the fabric under a set pressure difference.
- ISO 13934-1
Tensile strength, strip method
Measures the breaking strength of the fabric using the strip method.
- ISO 6330
Domestic washing
Applies a defined domestic wash cycle to assess wash durability and dimensional change.
- ISO 13937
Tear strength
Measures the force needed to propagate a tear in the fabric.
Third party laboratory testing can be arranged on request for a programme. Reports are issued by the testing laboratory, not by us, and we do not claim a certification this business has not been shown to hold.
What to supply before a bonded programme starts
A bonded jacket cannot be quoted accurately from a photograph. The six items below let us price the programme, run the bonding trial, and build the sample without guessing. Send them together and the sampling clock starts the same day.
- Construction drawing: panels, seams, pocket placement, and bonded zones.
- Measurements: a size chart with tolerances for each point of measure.
- Fabric spec: outer face, barrier, inner fleece, and fleece weight in GSM.
- Colour reference: a Pantone reference or a master swatch.
- Testing requirements: the methods you want reported.
- Packing instruction: polybag, hangtag, size sort, and carton count.
Read the wider capability in garment OEM and ODM manufacturing and logo windproof fleece jacket wholesale.
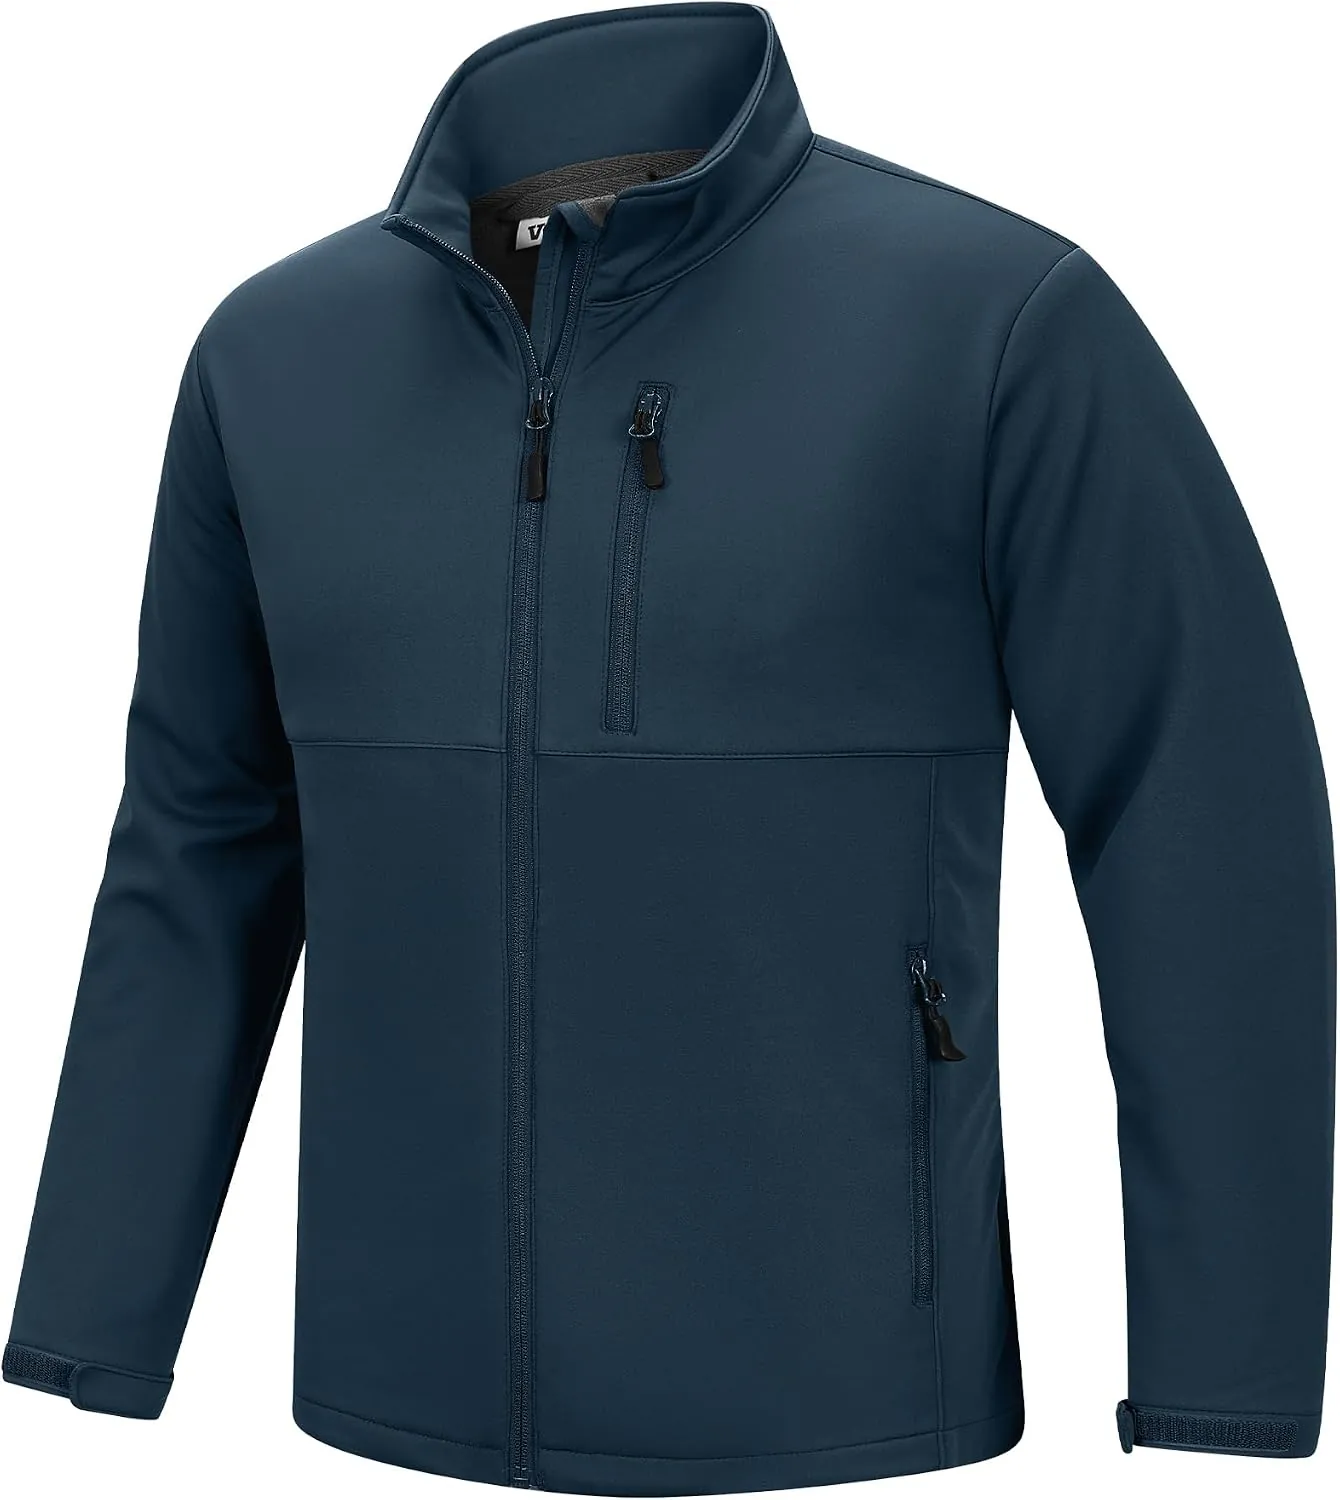
Care and wash instruction for a bonded laminate
A bonded jacket protects its own bond when it is washed and dried the way the laminate was built to be treated. The printed care label we produce for your programme always takes precedence, because the exact instruction depends on the faces and the membrane you specify.
Wash
Close all zippers and turn the jacket inside out. Wash cool on a gentle cycle with a mild detergent. Do not use bleach or fabric softener, which attack the adhesive and the fleece.
Dry
Tumble dry on low or line dry away from direct sun. High heat softens a bond before its time, so keep the dryer low and remove the jacket promptly.
Iron and store
Do not iron the membrane or the barrier film. Store the jacket clean, dry, and folded rather than compressed, away from a direct heat source.
Minimums, sampling, and lead time
The essentials a sourcing team asks for first. Final pricing depends on the laminate, quantity, and branding, so send the tech pack for a figure.
Low minimum per style and colourway. Pricing improves with volume, and a single pre production sample is available.
Sampling takes 3 to 5 days. Bulk production takes 7 to 12 days after approval, depending on quantity and colourways.
Official invoices in your chosen currency. Size sorted export cartons, polybags, and the packing instruction you specify.
Documentation and compliance for the programme
Documentation is provided per order, and certified yarn options are available where a programme calls for them. We describe what can be supplied rather than claiming a certificate this business has not been shown to hold.
- Certifications and standards overview
- Global Organic Textile Standard options
- Organic Content Standard options
- Environmental management documentation
Recycled polyester options certified under the Global Recycled Standard are available with transaction certificates supplied per order, and certified yarn options can be specified for a programme.
For buyers who ship into regulated markets, we prepare export cartons and shipping documents and can coordinate third party laboratory testing on request. To confirm what your order needs, reach the team through contact us or send the tech pack to the manufacturing desk.
From tech pack to packed cartons
A bonded programme has one extra gate that a plain fleece programme does not, the bonding trial, and it sits before the bulk run so a problem with the bond is found on a swatch rather than on a thousand panels.
- 1
Tech pack review
We read the drawing, the measurements, and the laminate spec, then confirm the faces, film, and weight band.
- 2
Bonding trial and sample
We bond a trial swatch on the actual faces, agree the bond, then build a sample.
- 3
Bulk bonding
The laminate is bonded to spec and released to cutting after the cure window.
- 4
Cut, sew, and brand
Panels are cut, sewn with SBS zippers, and branded with Tajima embroidery.
- 5
Inspect and pack
Each jacket is inspected, the care label applied, and the order packed to instruction.
Bonded fleece windproof jacket FAQ
The questions a technical buyer asks before specifying a bonded laminate.
What does bonding mean in a bonded fleece windproof jacket?
Bonding joins the outer face, the barrier film, and the inner fleece into one three layer laminate using an adhesive system under heat and pressure. The bond covers the full surface, so the layers move as one panel.
Is the windproof layer a membrane or a coating?
A bonded programme normally uses a membrane film laminated between the faces. A membrane is a separate layer inside the laminate, while a coating is applied to the back of the outer fabric.
How is breathability handled in a bonded laminate?
Breathability depends on the membrane. A windproof film blocks air but does not transfer vapour, which suits cold, low exertion use. A breathable membrane transfers vapour while resisting wind for active use.
What causes delamination and how do you guard against it?
Delamination is usually caused by heat exposure, a low grade adhesive, or repeated washing. We control lamination temperature and pressure, match the adhesive to the faces, run a bonding trial, and honour the cure time before cutting. The tech pack should name a bond peel strength target and its test method.
How does a bonded laminate hold up to repeated washing?
Wash durability depends on the adhesive system, the cure, and the care routine. We build to the wash care in your tech pack and can arrange ISO 6330 domestic washing assessment through a third party laboratory.
What is the minimum order for a bonded windproof fleece jacket?
The minimum is 20 pieces per style and colourway. We also produce a pre production sample so your team can inspect the laminate, the bond, the fit, and the branding.
Can we get samples, lab dips, and fabric swatches before production?
Yes. Sampling takes 3 to 5 days. We supply lab dips and fabric swatches, plus a bonded sample to check the hand, the loft, and the bond. Nothing is cut until both are approved.
Can you arrange third party laboratory testing for our programme?
Yes. Third party laboratory testing can be arranged on request, and reports are issued by the testing laboratory, not by us. Buyers commonly request ISO 811, ASTM D737, ISO 13934-1, ISO 6330, and ISO 13937.
What must we supply in the tech pack?
A tech pack should carry the construction drawing, the measurement chart, the fabric and laminate spec, a colour reference, the testing requirements, and the packing instruction.
What is the production lead time?
Sampling takes 3 to 5 days. Bulk production takes 7 to 12 days after sample approval, depending on quantity and colourways. Bonding trials and lab dips sit inside that window.
Related fleece and windproof programmes
Explore the neighbouring programmes before you lock the laminate, so the construction you specify sits correctly against the rest of the range.
Request a bonded fleece windproof jacket quote
Send your construction drawing, measurements, laminate spec, colour reference, testing requirements, and packing instruction. Our manufacturing desk in Tagum City replies with a costed programme, a sampling schedule, and the bonding trial plan.